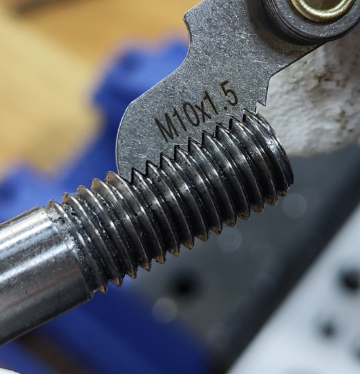
Broken taps and other threaded tools can create difficult problems in machining and maintenance. When a tap snaps inside a drilled hole, the remaining fragment may obstruct further work and threaten an otherwise usable component. Removing the fragment without damaging the surrounding material can be challenging, especially when the workpiece is expensive, difficult to replace, or already partly machined.
Electrical discharge machining, commonly known as EDM, is one method that can be considered for removing certain broken conductive tools.
Why Broken Taps Are Difficult to Remove
Taps are used to create internal threads in prepared holes. They can break because of excessive torque, incorrect alignment, unsuitable cutting conditions, inadequate lubrication, worn tooling, or chips that become trapped during machining.
Once a tap breaks, its hardened material can be difficult to drill using conventional tools. Attempts to force or extract the fragment may damage the existing threads or cause additional breakage.
The right recovery method depends on the tap material, its position, the workpiece material, the depth of the hole, and whether the component can be moved to a dedicated machine.
Understanding EDM-Based Removal
Electrical discharge machining removes conductive material through controlled electrical discharges between an electrode and the workpiece. The process does not rely on a conventional cutting edge to remove material in the same way as drilling or milling.
For suitable broken-tool applications, EDM can be used to erode material from the trapped fragment, helping create a path for its removal. The exact procedure depends on the equipment, electrode arrangement, fragment geometry, and workpiece.
EDM is not appropriate for every material or situation. Conductivity, access, fragment depth, and the required condition of the original hole must all be considered.
Businesses evaluating portable recovery equipment can review the Clyertek portable EDM broken tap remover as a reference when comparing solutions for selected broken-tool removal tasks.
When Portable Equipment May Be Useful
Repairing expensive workpieces
A broken tap can jeopardise a component that has already undergone substantial machining. Replacing the whole part may be costly, especially when the component has a long lead time or contains several completed operations.
A suitable EDM removal process may offer a way to recover selected parts, but the feasibility should be assessed before work begins. If the fragment is deeply embedded or access is restricted, the operation may require specialised setup or technical support.
Maintenance in different work areas
Portable equipment may help workshops handle recovery tasks without moving every component to a central machining station. This can be useful when a workpiece is large or integrated into a larger assembly.
However, portability does not eliminate the need for a stable setup, appropriate electrical arrangements, safe access, and correct workpiece positioning. Confirm that the specific application can be handled within the equipment’s operating limits.
Reducing avoidable scrap
When a component can be recovered safely, removing a broken tool may prevent unnecessary disposal. The economic benefit depends on the value of the part, the time required for recovery, and the likelihood of preserving the original thread.
Recovery should not be assumed successful until the hole and surrounding material have been inspected.
Preparing for a Broken-Tool Removal Job
Before using EDM, identify the workpiece material and the broken tool. Confirm that the materials and fragment are compatible with the proposed process.
Assess the fragment’s depth, orientation, size, and accessibility. Determine whether the workpiece can be secured adequately and whether the operation could affect nearby surfaces or precision features.
The operator should also establish the required end condition. In some cases, the goal is to remove the fragment while preserving the original threads; in others, the hole may need additional inspection or rework before it can be used again.
Photographs, component drawings, and details about the original machining operation can help a qualified technician evaluate the situation.
Preventing Further Damage During Recovery
The removal process should be controlled and monitored carefully. Incorrect positioning or unsuitable operating parameters may affect the workpiece or fail to remove the fragment effectively.
Follow the equipment manufacturer’s instructions and use the appropriate electrode and setup for the job. Avoid improvising with unapproved tools or attempting to force the fragment out after material has been removed.
After extraction, inspect the hole and threads for damage, remaining debris, or dimensional changes. Depending on the component’s purpose, additional inspection may be required before it returns to production.
Preventing Future Tap Breakage
Broken-tool recovery is valuable, but prevention can reduce interruptions and rework. Machining teams should review the causes of repeated tap failures.
Useful preventive measures include selecting the correct tap for the material, checking tool condition, maintaining appropriate alignment, using suitable cutting parameters, and ensuring that lubrication and chip evacuation meet the operation’s requirements.
Training operators to recognise excessive resistance or unusual cutting behaviour can also help prevent failures. Where appropriate, review the hole preparation and thread specifications before starting the tapping operation.
Cost and Workflow Considerations
When comparing recovery methods, consider the component’s replacement value, downtime, labour, setup time, equipment cost, and risk of damage. Conventional extraction may be suitable for some cases, while EDM may be worth investigating when hardened fragments are difficult to remove mechanically.
The decision should be based on the individual job rather than a universal assumption that one method is always best. A recovery procedure should also include inspection and approval before the component is returned to service.
Frequently Asked Questions
1. Can EDM remove every broken tap?
No. Feasibility depends on the fragment, workpiece material, accessibility, and equipment capabilities. The specific case should be assessed before recovery begins.
2. Will broken-tap removal preserve the original threads?
It may be possible in suitable cases, but preservation is not guaranteed. The hole and threads should be inspected after the fragment is removed.
3. What information helps determine the right removal method?
Useful details include the workpiece material, tap size, fragment depth, hole location, accessibility, and the component’s value and precision requirements.
Conclusion
A broken tap can turn a routine machining operation into a costly recovery task. EDM offers a potential solution for selected conductive fragments that are difficult to remove with conventional tools. Careful assessment, controlled operation, and post-removal inspection are essential to protect the surrounding component. Combining an appropriate recovery method with better tapping practices can help machining businesses reduce avoidable scrap and maintain more dependable production workflows.